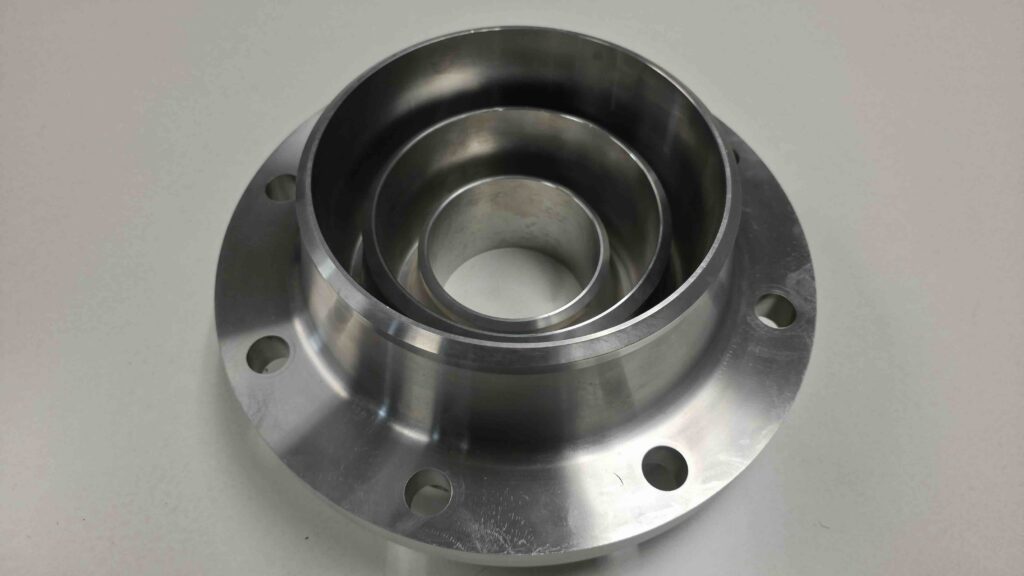
A weld neck flange starts as a solid steel billet and ends as a precisely machined component with a tapered hub and beveled weld end. The manufacturing process of weld neck flanges includes heating, forging, and machining steps. Those steps determine the flange’s grain structure and dimensional accuracy. In this guide, we cover the manufacturing sequence and explain why the forging process matters for the flange’s performance under pressure.
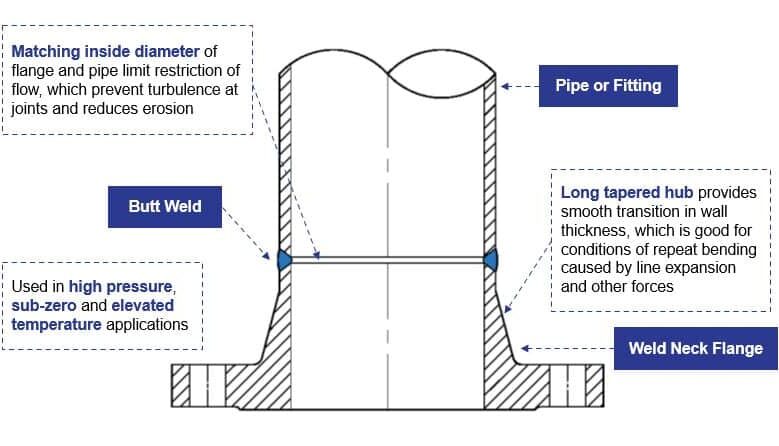
Weld neck flanges are manufactured by a forging process rather than casting or cutting from plate. Forging aligns the internal grain structure of the steel along the contour of the finished part. This process produces a denser, tougher, and more uniform structure than plate stock. Casting, on the other hand, pours molten steel into a mold and can leave internal porosity. It’s typically used for some specialty or large custom shapes, but not for standard pressure-rated weld neck flanges under ASTM A105 or A182.
The Manufacturing Sequence
The forging process for a weld neck flange follows a consistent sequence, regardless of whether the finished part is carbon steel or stainless steel.
1. Raw Material Preparation
The manufacturing process begins with round or square steel billets in the target grade, typically ASTM A105 for carbon steel or A182 for stainless and alloy steel. Mill certificates document the chemical composition of each heat before the billet moves to production.
2. Cutting to Length
After the first step, billets are typcially saw cut to the specific length needed for the finished flange. This step helps minimize waste and ensure consistent volume for the forging step that follows.
3. Preheating
The cut billet is heated in a furnace above the steel’s recrystallization temperature, then soaked until its internal temperature is entirely uniform. Reaching this heat significantly reduces the steel’s yield strength, making it pliable enough to shape without risk of cracking.
4. Forging
The forging process starts with shaping the heated billet into the rough flange form using a press or hammer – a step known as “hot working.” Standard weld neck flanges are typically manufactured using ring rolling. In this process, the heated billet is upset-forged by axial compression, pierced to create a hollow blank, and then expanded between main and pressure rolls. This rolling step shapes the final ring while refining the metal’s circumferential grain structure. Larger or non-standard weld necks may instead use open-die forging. Both of those methods produce a continuous, directional grain flow that follows the contour of the hub and flange face, giving forged components a distinct structural advantage over plate-cut alternatives.
5. Machining
The as-forged flange is turned on a CNC lathe to bring the face, hub taper, and outside diameter to final dimensions. Bolt holes are then drilled to match the specified bolt circle (like the designs governed by ANSI/ASME B16.5 or B16.47). Facing operations also cut the raised face or flat face sealing surface and any required serrations.
6. Heat Treatment
Depending on the class and size, the flange may be supplied in an as-forged state or undergo heat treatments such as normalizing or tempering to refine the grain structure to meet the mechanical property requirements of ASTM A105 or A182. Larger, higher-pressure-class flanges are more likely to require heat treatment than small, low-pressure-class parts.
7. Inspection, Marking, and Finishing
In the final stage of manufacturing, finished flanges are inspected for dimensional accuracy and surface defects. Once approved, each flange is stamped with the material grade, heat number, and any other required part markings. Certified mill test reports accompany each heat, documenting the chemistry and mechanical properties confirmed through testing.
Production Method Comparison
The distinction matters structurally, not just procedurally. A forged weld neck flange has a continuous grain structure running from the bolt face through the tapered hub and into the weld bevel – precisely where operational stress peaks once the flange is welded to pipe and put into service. This grain continuity allows a forged weld neck flange to withstand repeated pressure cycling, thermal expansion, and vibration, preventing fatigue cracks from developing at the hub-to-pipe transition.
Production Method | Grain Structure | Typical Use |
Forging (ring rolling or open-die) | Continuous, directional grain flow | Standard weld neck flanges, ASTM A105/A182 |
Casting | Grain structure set by mold, risk of internal porosity | Specialty shapes, valve bodies, some large fittings |
Plate cutting | No directional grain refinement | Slip-on and blind flanges in lower-pressure service |
Common Materials Used in Manufacturing
Carbon steel weld neck flanges are typically forged from standard material like ASTM A105 billet, while stainless steel versions use ASTM A182 most commonly in grades F304/F304L or F316/F316L. Both standards specify the chemical composition, mechanical properties, and heat treatment conditions for the finished forging. Other material grades can be specified based on application and other requirements.
| Grade | Product Form | Typical Service |
| ASTM A105 | Forged carbon steel | General process and power piping, ambient to 800°F |
| ASTM A182 F304/F304L | Forged stainless steel | Corrosion resistance, moderate-temperature process piping |
| ASTM A182 F316/F316L | Forged stainless steel | Higher corrosion resistance, chloride and marine environments |
| ASTM A182 F11, F22, F91 | Forged alloy steel | High-temperature steam and process piping above carbon steel limits |
| ASTM A350 LF2 Class 1 | Forged Carbon Steel | Low-temperature service (down to -20°F) with Notch Toughness testing requirements |
Conclusion
That full process described in this guide is what gives a forged weld neck flange the continuous grain structure and dimensional accuracy that plate-cut or cast alternatives cannot match. API International supplies weld neck flanges forged from A105 carbon steel and A182 stainless steel, machined to ANSI/ASME B16.5 and ANSI/ASME B16.47 dimensions. Explore our full range in the online product catalog, or contact us for custom machining on nonstandard sizes. Get connected with a dedicated sales representative today, or call us at 503.692.3800.
Frequently Asked Questions
Are weld neck flanges forged or cast?
Standard weld neck flanges are forged, not cast. Forging aligns the internal grain structure along the shape of the part, producing a denser and more uniform structure than casting or plate cutting.
What is ring rolling in flange manufacturing?
Ring rolling is a forging method where a heated billet is upset-forged, pierced into a hollow blank, and rolled between main and pressure rolls to expand it into its final ring shape. This method produces continuous grain flow in the circumferential direction, which is the standard method for producing weld neck flanges.
What steel grade is used to forge weld neck flanges?
ASTM A105 is the standard carbon steel grade, and ASTM A182 (F304/F304L, F316/F316L) is used for stainless steel weld neck flanges.
Why does forging matter for a weld neck flange's performance?
Forging produces a continuous grain structure through the hub and into the weld bevel, which is where stress concentrates once the flange is in service. This grain continuity gives forged flanges superior fatigue resistance under pressure cycling and thermal expansion compared to cast or plate-cut alternatives.
Do all weld neck flanges require heat treatment?
Not always. Smaller, lower-pressure-class flanges may be supplied as-forged, while larger sizes and higher pressure classes typically require normalizing or tempering to meet the mechanical property requirements of the specified ASTM grade.